Industrial Pumping Solutions
Engineered for Performance
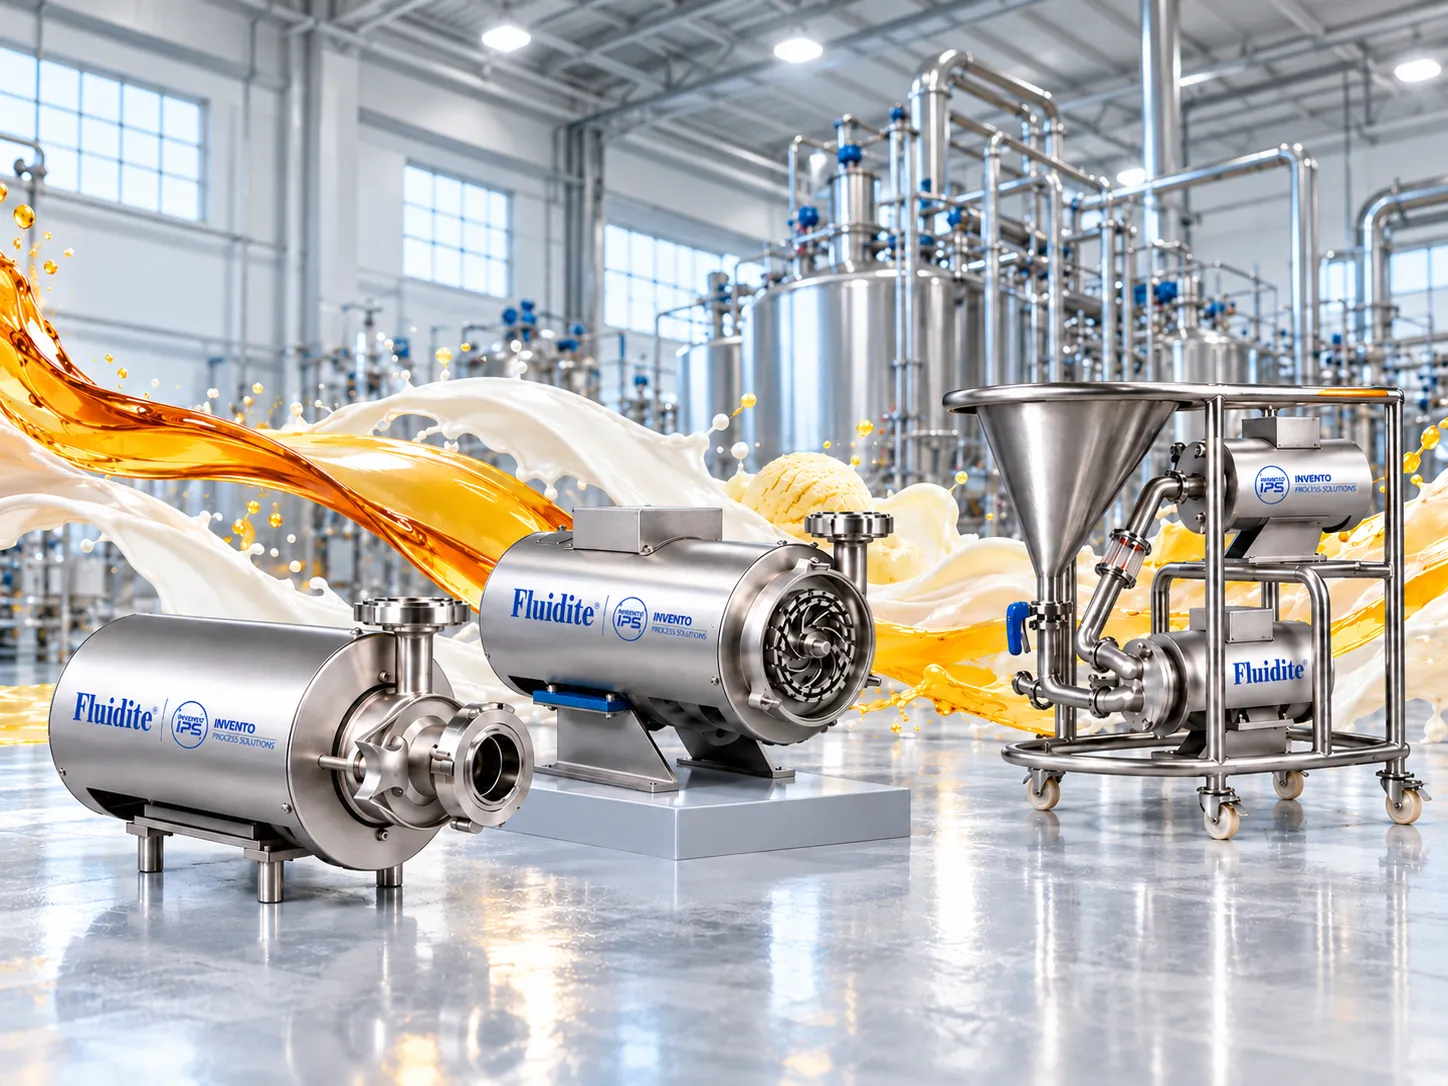
Comprehensive range of sanitary pumps including Lobe, Centrifugal, and Gear pumps for viscous, shear-sensitive, and hygienic fluids.

Consistent flow. Efficient transfer. Dependable operation.
Centrifugal pumping solutions engineered for reliable liquid transfer across industrial processes, utilities, and fluid handling applications.
Products
Six specialized product lines. One trusted manufacturer.

Engineered for Performance
Comprehensive range of sanitary pumps including Lobe, Centrifugal, and Gear pumps for viscous, shear-sensitive, and hygienic fluids.

Innovative Excellence in Process Engineering
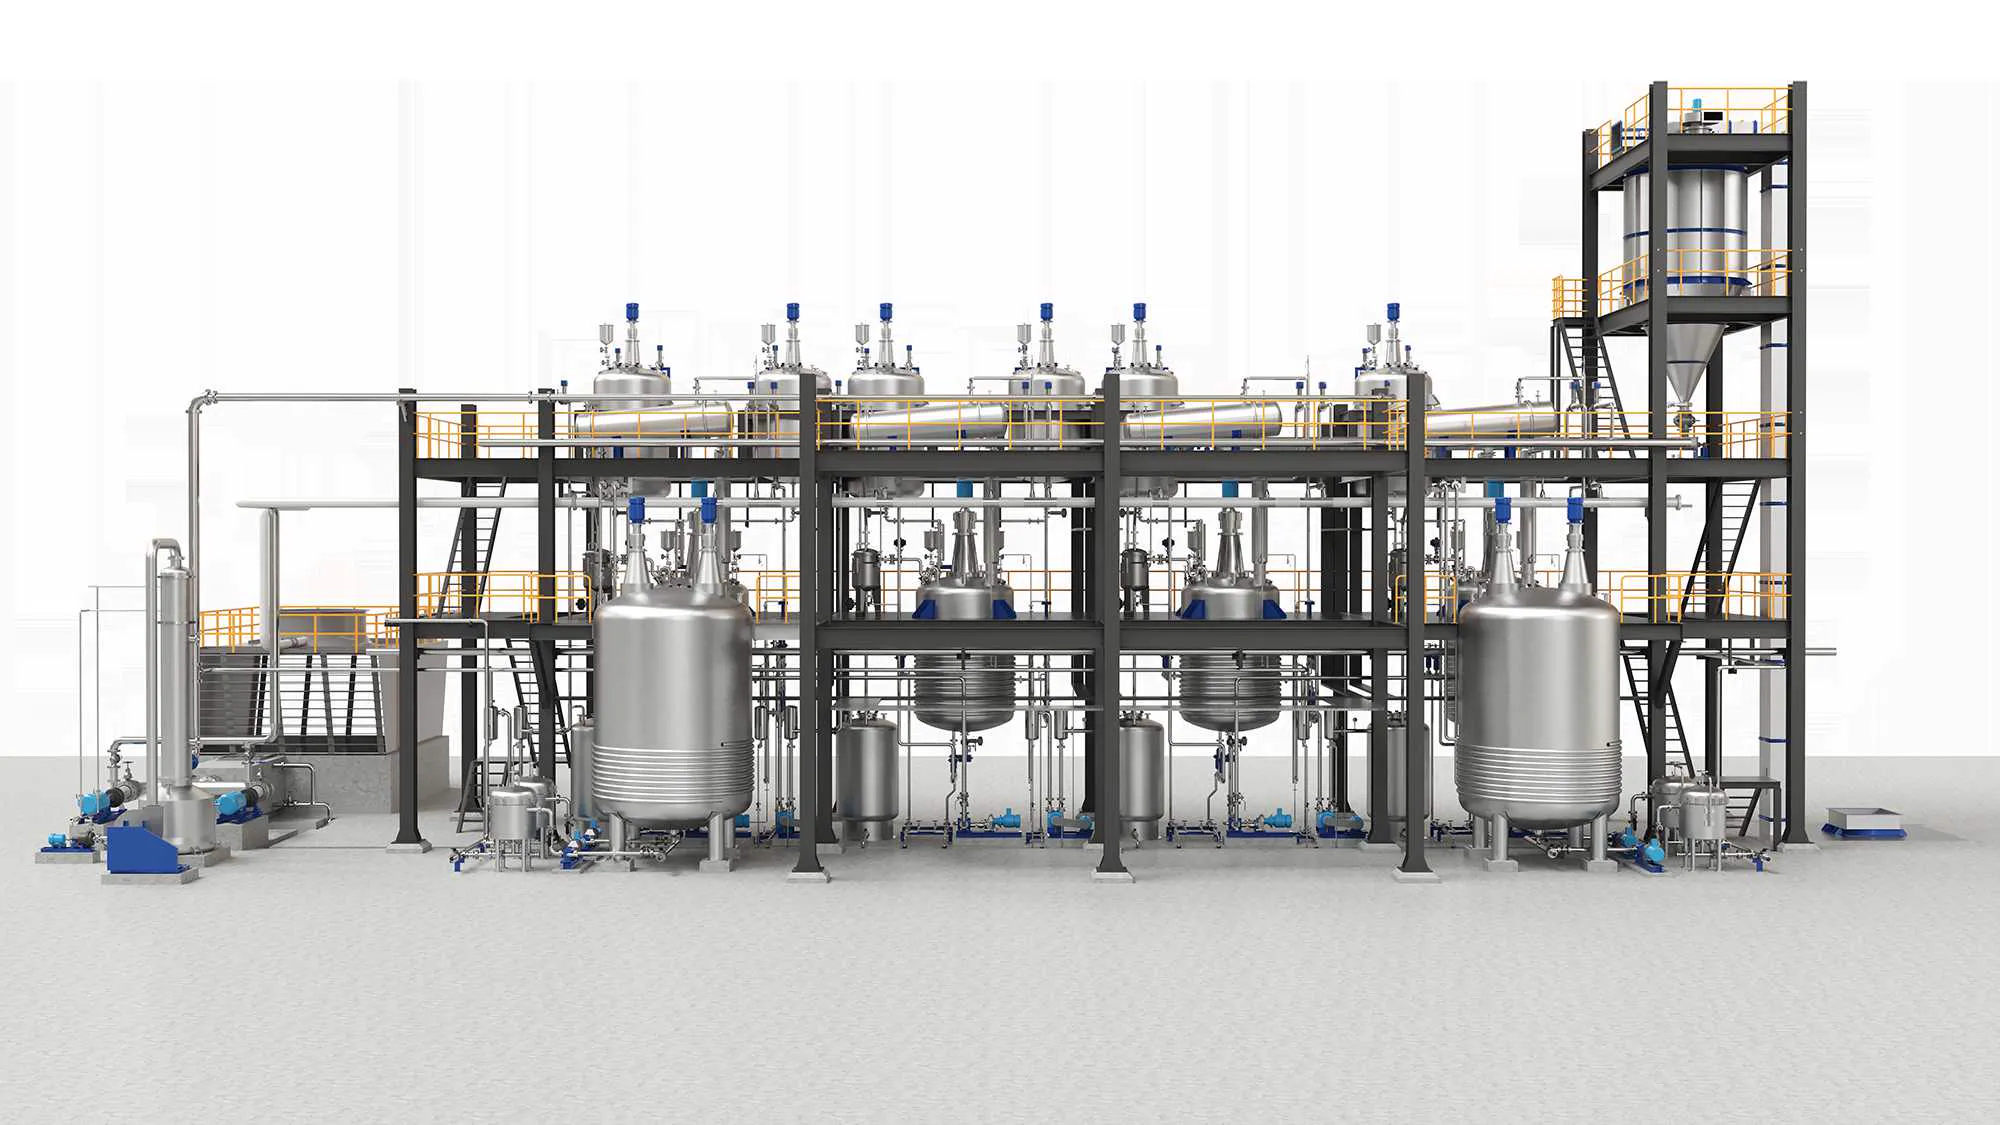
Complete range of process equipment — reactors, heat exchangers, blenders, dryers, filtration, and turnkey plants for pharma, chemical, and food industries.

Connected, Controlled & Data-Informed Process Operations
Advanced PLC panels, MCC power distribution, SCADA architectures, and digital monitoring solutions for precise operational control and visibility.

Integrated Plant Solutions from Design to Commissioning
Custom-engineered turnkey process plants including acid dilution, ethanol distillation, solvent recovery, and dairy & processing plants with complete process integration.

Flexible Platforms for Process Development & Scale-Up
Custom-engineered pilot plants and laboratory-scale reactor platforms for catalyst evaluation, reaction kinetics, process intensification, and scale-up studies.

Precision Equipment for Pharmaceutical Manufacturing
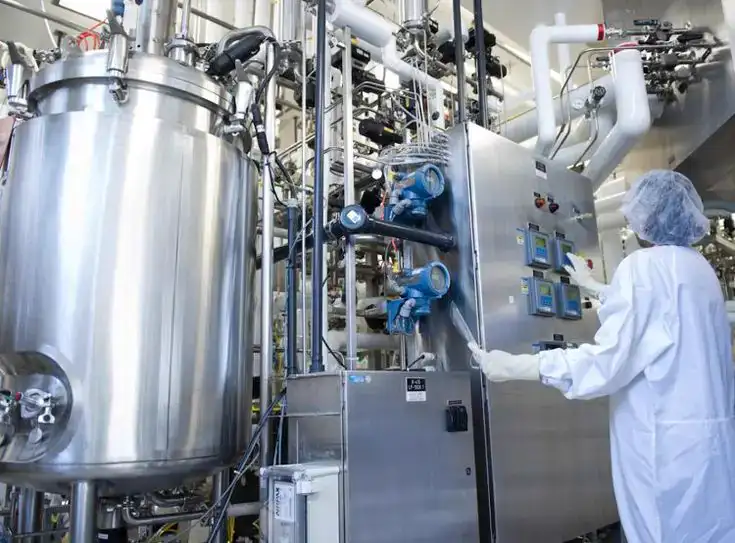
Precision pharmaceutical equipment including Rapid Mixer Granulators, Multi Mills, Paste Kettles, Vibro Sifters, and validated CIP systems for sterile and formulation facilities.
Applications

Process equipment and fluid handling solutions for upstream and downstream oil and gas operations.

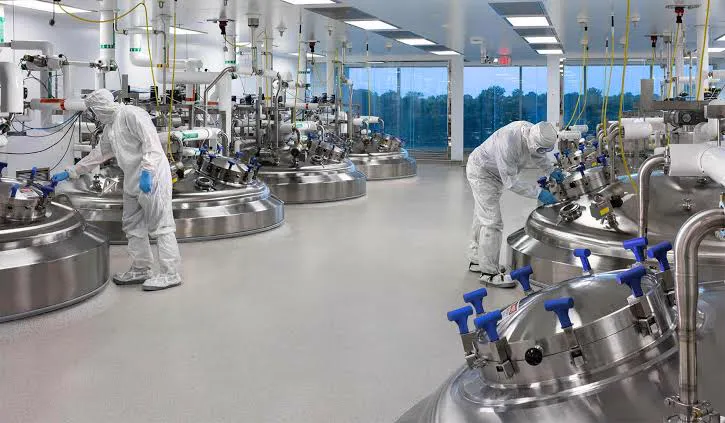
GMP-compliant equipment for pharmaceutical manufacturing, API processing, and sterile applications.

Corrosion-resistant process equipment for specialty chemical manufacturing and handling.

3-A sanitary compliant equipment for milk, cream, yoghurt, butter, and cheese processing.

Hygienic fluid transfer and processing equipment for juice, soft drink, and beverage production.

Laboratory and pilot-scale systems for research institutes and R&D facilities.

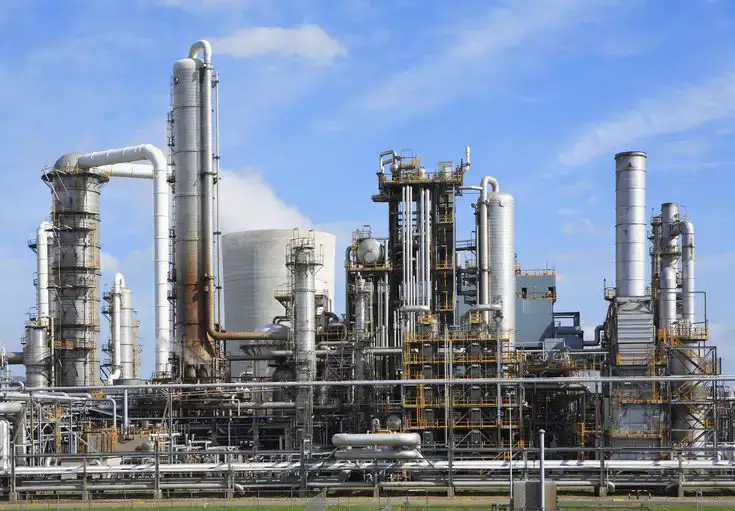
Heavy-duty process equipment for petrochemical refining and processing plants.

Precision fluid handling for body lotions, shampoos, face creams, and personal care formulations.
Advantages
All products engineered to meet the highest hygienic and sanitary standards.
Advanced technology and process engineering expertise behind every product.
Built for continuous operation with long, maintenance-free service life.
Pre and after-sales support with committed on-time delivery.
Send Enquiry
Fill in the form and our team will get back to you within 24 hours.